Standard vs tight CNC tolerance
Tolerance is the total allowed deviation from a dimension. Specifying every feature to the tightest possible number raises cost dramatically, so a good drawing uses general tolerance for non-critical features and tight tolerances only where function demands. Our default for CNC milled and turned parts is ISO 2768-mK (medium / coarse), which covers most mechanical assemblies, and we routinely hold ±0.01 mm on critical features with high-precision setups.
What ISO 2768 covers
ISO 2768 is a general tolerance standard for linear and angular dimensions, form and position when no individual tolerance is shown. For example, under the "m" class a dimension between 30 and 120 mm allows ±0.2 mm, and finer dimensions less. Marking a drawing "ISO 2768-mK" avoids over-dimensioning while setting a clear, internationally recognised default. Hole/shaft fits that move, seal or locate should instead be given explicit tolerances (e.g. an H7 bore, an h6 shaft).
What determines the tolerance you can achieve
- Material and stability: plastics and soft metals move more; thin walls and long parts deflect under cutting force.
- Part geometry and size: the larger and more slender the feature, the harder it is to hold a tight number.
- Number of setups: machining faces in one clamping (3+2 or 5-axis) avoids alignment error — see 5-axis machining.
- Machine, tooling and temperature: CMM-verified, climate-controlled inspection is needed for ±0.01 mm work.
- Post-processing: heat treatment, plating and anodising slightly move dimensions; critical features are finished after treatment.
Surface finish: understanding Ra
Ra is the average roughness of a surface in micrometres (µm). Lower Ra means smoother, more expensive to produce. Typical as-machined values are Ra 1.6–3.2 for milling and Ra 0.8–1.6 for turning. A fine finishing pass, polishing or grinding can reach Ra 0.4–0.8, and mirror/polished stainless can go lower. Ra 3.2 is fine for most structural surfaces; Ra 1.6 is common for visible and mating surfaces; Ra 0.8 or finer is specified for sealing surfaces, bearings and high-fatigue parts. In imperial units, 1.6 µm is roughly 63 µin and 0.8 µm is 32 µin.
Match the callout to the function
- General structural parts: ISO 2768-m, Ra 3.2 — no extra cost.
- Mating and locating surfaces: explicit ±0.02–0.05 mm, Ra 1.6.
- Sealing, bearing and high-precision features: ±0.005–0.01 mm, Ra 0.8 or finer, with a defined GD&T callout.
- Use GD&T (geometric tolerancing) — flatness, perpendicularity, true position, concentricity — when the relationship between features matters more than a single size.
Inspection and CMM reports
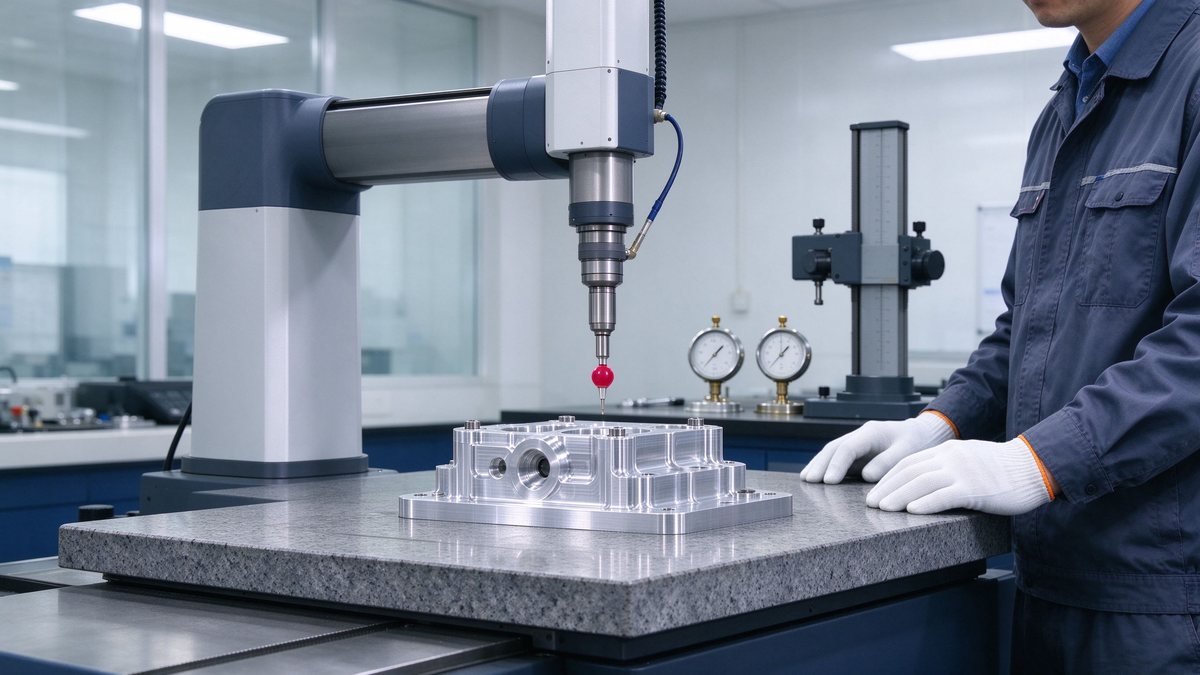
We verify dimensions with a CMM (coordinate measuring machine), height gauges, micrometers, bore gauges and pin/thread gauges in a dedicated metrology area. On request we provide a first-article inspection (FAI) report and a CMM dimensional report with measured values, plus material mill test certificates (EN 10204 3.1) — important for stainless steel, medical and aerospace parts. Mark critical dimensions on the drawing and we will plan inspection around them. Send your drawing for a quote with a tolerance review, or read about how anodising affects dimensions.